The job at line end
Line-end sealing is cyclic by nature: seal, cut, advance, repeat — against a line that keeps producing. The knife system has to keep seal quality constant across a shift, cope with the film range the line actually runs, and recover cleanly after a film change or a stop. That's a control problem as much as a heating problem, which is why the knife and controller ship as one matched system.
For machine builders
We supply OEMs the same hot-cutting knife systems we build into our own equipment, with the integration work done properly:
- Mounting interfacesBlade carrier and station dimensions matched to your machine's sealing position — from photographs and dimensions, not assumptions.
- Control integrationManual 0–10 current setting for operator-tuned lines, or remote setpoint driven by your PLC; status and fault signals available.
- DocumentationInterface drawings and I/O descriptions your engineers can work from — in English if your line goes overseas.
- Random & aftermarket sparesA first-year spares list classified by downtime risk, and repeat supply of wear parts for machines already in the field.Talk to us about terms.
What we need from you
- FilmStructure (PE, PP, laminate), width and thickness range.
- CycleSeal/cut cycle rate and whether line speed varies.
- InterfaceMounting points, available space, control signal preference.
- For OEMsEstimated annual volumes — both machines and spare knives — so we quote the program, not just the unit.
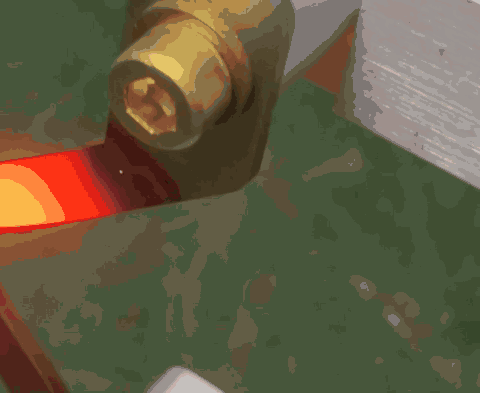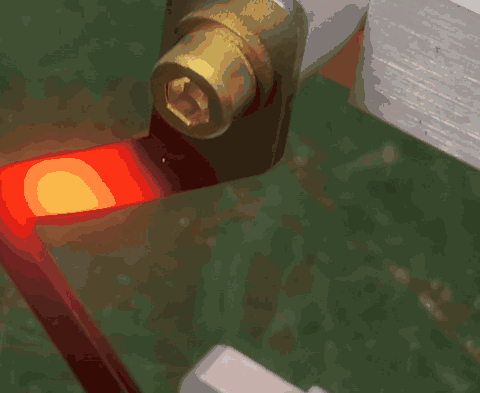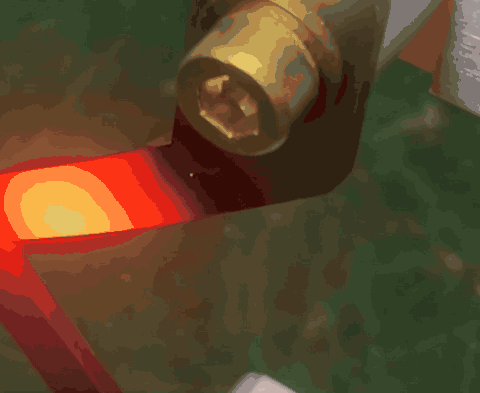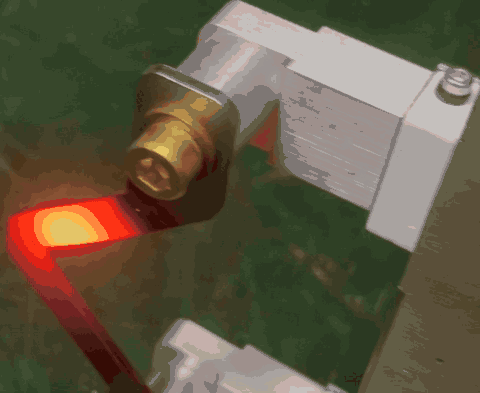 Sealing edge at working temperature — recorded from our demo unit